Vacuum Casting Services
Plasticpartsmfg delivers precision polyurethane vacuum casting (urethane casting) from Shenzhen, China. Built for engineering teams, hardware startups, and product developers requiring 10 to 500+ production-grade plastic parts without expensive injection tooling.
Typical Batch
10–500 pcs
Standard Lead Time
7–10 Days
Mold Lifespan
15–25 Shots
Tolerances
±0.15 mm / 100mm
Fast Engineering Review Shenzhen Direct
- No Hard Tooling Required: Silicone molds cut upfront setup costs by over 70% vs steel molds.
- Engineering-Grade Resins: Simulates ABS, Polycarbonate, PP, POM, and rubber/TPE (Shore 30A to 85D).
- Finishing Flexibility: Mold-tech textures, high-gloss polish, custom Pantone matching, and brass threaded inserts.
- Bridge Production: Supply functional components during injection mold design and validation cycles.
Technical Capabilities & Process Boundaries
Vacuum casting parameters verified on daily client production runs at Plasticpartsmfg.
| Parameter | Standard Specification | Engineering Notes |
|---|---|---|
| Simulated Resins | ABS-like, PC-like, PP-like, PMMA-like (Optically Clear), Rubber-like (Shore 35A–85A), Fire-Retardant (UL94-V0) | Polyurethane formulations matched to mechanical testing criteria. |
| Dimensional Tolerance | ±0.15 mm for first 100 mm, ±0.05 mm for each additional 100 mm | Influenced by master pattern accuracy, shrinkage factor, and geometry. |
| Max Part Dimensions | Up to 1,900 mm × 900 mm × 750 mm | Chamber-capacity dependent; structural ribbing advised for large spans. |
| Min Wall Thickness | 1.0 mm (0.75 mm in localized rib sections) | Adequate flow paths prevent short shots in high-viscosity resins. |
| Inserts & Overmolding | Brass threaded inserts, stainless pins, dual-durometer overmolding | Pre-heated inserts placed in silicone mold cavity prior to casting. |
| Surface Finishes | VDI / Mold-Tech Spark, Mirror Polish, Custom Texture, Matte, Soft-Touch Paint | Surface finish is replicated directly from the CNC/SLA master pattern. |
When Vacuum Casting Outperforms Alternatives
Selecting the right process reduces upfront tooling exposure while meeting mechanical and aesthetic requirements.
Vs. 3D Printing (SLA / SLS)
Vacuum casting delivers isotropic mechanical strength, actual production resin properties (ABS, PP, Rubber), and bubble-free optical clarity that additive processes struggle to match at unit scales of 15–100 pieces.
Best for: Rigorous functional & drop testing
Vs. CNC Machining Plastics
Deep ribs, internal undercuts, thin walls, and complex draft profiles become costly when CNC milled. A single SLA master pattern allows silicone molding to replicate internal features effortlessly.
Best for: Intricate enclosures & thin-wall covers
Vs. Hard Injection Tooling
Steel and aluminum molds take 4–7 weeks and thousands in capital. Vacuum casting silicone tooling delivers the first 20–50 verified units in 7–10 days, securing customer demo units and pilot verification without financial lock-in.
Best for: Pilot batches & design iterations
Vacuum Casting Solutions & Process Articles
Browse targeted technical articles, material case studies, and engineering guidelines for urethane casting projects.
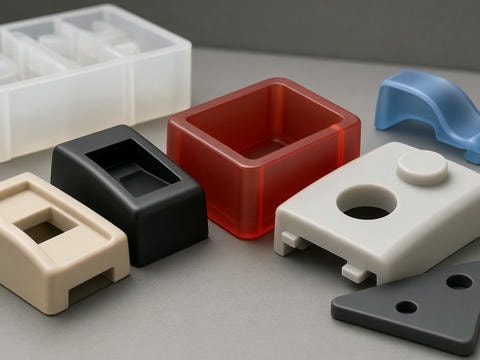
Custom Urethane Casting Services | Low-Volume Production | Plasticpartsmfg
Get high-quality custom urethane casting parts from Plasticpartsmfg. Ideal for functional prototypes, bridge production, and small-batch runs. Upload your CAD files today.
View details →
Low-Volume Vacuum Casting Services | Rapid Plastic Parts | Plasticpartsmfg
Get professional low-volume vacuum casting services for plastic parts. Ideal for prototypes, functional testing, and bridge production. Upload your CAD for a quote.
View details →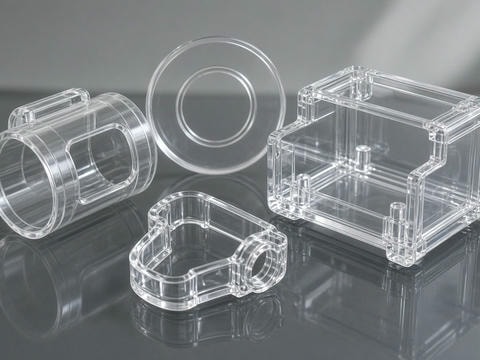
Clear Vacuum Casting Services | Low-Volume Transparent Plastic Parts
Get high-quality clear vacuum casting parts for prototypes and low-volume production. We support custom materials, surface finishes, and rapid turnaround.
View details →Dimensional & Cosmetic Verification
Every polyurethane batch undergoes rigorous dimensional, cosmetic, and physical checks before packaging.
Master Pattern Check
CMM verification and optical scanning of SLA/CNC masters ensure precision before silicone encapsulation.
Vacuum De-Gassing
Dual-chamber vacuum degas process prevents micro-voids, bubbles, and surface pitting in thick sections.
Color & Gloss Measure
Spectrophotometer verification against customer Pantone/RAL standards and defined gloss levels.
Custom Export Crating
Component-level protective bagging, foam cells, and sturdy export cartons avoid transit warping.
Request Your Vacuum Casting Quote
Send your STEP, IGES, or PDF files. Our manufacturing engineers in Shenzhen evaluate part geometry, suggest suitable PU resin grades, and provide a competitive quote with DFM feedback within 12–24 hours.
Direct Engineering Support
Communicate directly with engineers who inspect your 3D geometry.
Flexible Quantity Commitments
From a single test run of 5 units to bridge production batches of 500+.
Comprehensive Secondary Processing
Pad printing, brass inserts, ultrasonic staking, and light assembly in-house.
Confidentiality Assured
We execute non-disclosure agreements (NDAs) routinely before review of customer IP and proprietary 3D CAD models.