Custom PA Parts Manufacturing Services
Based in Shenzhen, China, Plasticpartsmfg delivers on-demand Polyamide (PA6, PA66, PA12) component manufacturing for functional prototypes, bridge tooling, and low-to-medium volume production. Send your STEP, IGES, or 2D technical drawings for precision tolerance analysis and rapid production quotation.
Technical Specification Matrix Engineering Verification
Material Selection & Machinability Guide for Polyamide Components
Polyamide is chosen for its superior mechanical strength, friction resistance, and thermal endurance. Selecting the correct PA compound and manufacturing route is critical to avoiding moisture distortion and thermal deformation during operation.
PA6 / Cast Nylon
Excellent damping characteristics and impact resistance. Highly suitable for structural gears, rollers, guide rails, and heavy-load wear strips where mechanical vibration absorption is critical.
- Tensile Strength: ~78 MPa
- Melting Point: ~220°C
- Process: CNC Machining & Casting
PA66 / PA66-GF30
Higher stiffness, lower creep, and elevated heat deflection temperatures. Glass-fiber reinforcement dramatically boosts rigidity for engine compartments, pump housings, and terminal blocks.
- Tensile Strength: ~85–175 MPa
- Melting Point: ~260°C
- Process: Injection Molding & CNC
PA12 / SLS Nylon
Lowest moisture absorption among commercial polyamides, ensuring superior dimensional stability in humid environments. The prime material for SLS additive manufacturing and complex conduit routing.
- Moisture Absorption: < 0.5%
- Melting Point: ~178°C
- Process: SLS/MJF 3D Printing & Extrusion
Custom PA Parts: Manufacturing Disciplines
Explore our targeted production capabilities for Polyamide components. From single prototype validation to volume tooling and continuous extrusion profiles.
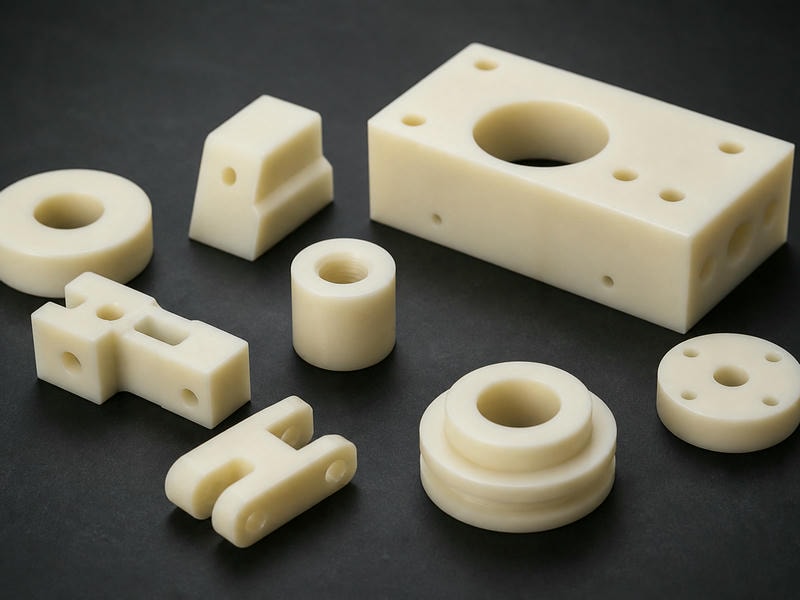
PA CNC Machining Services | Custom Nylon Parts - Plasticpartsmfg
Professional PA CNC machining services for prototyping and low-volume production. We deliver precision Nylon components with tight tolerances for industrial use.
View details →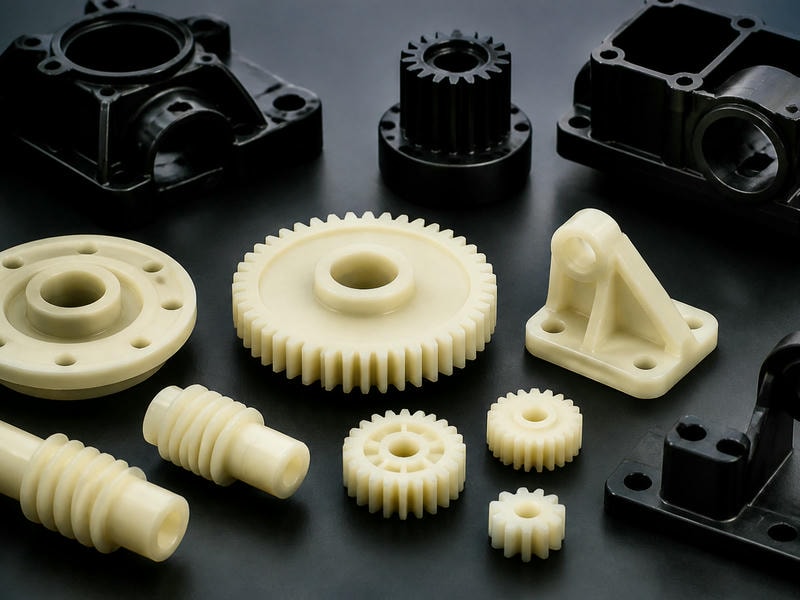
Custom PA Injection Molding Services | Plasticpartsmfg
Plasticpartsmfg provides precision PA (nylon) injection molding services in Shenzhen. Supporting prototypes to mass production. Upload your CAD files for a quote.
View details →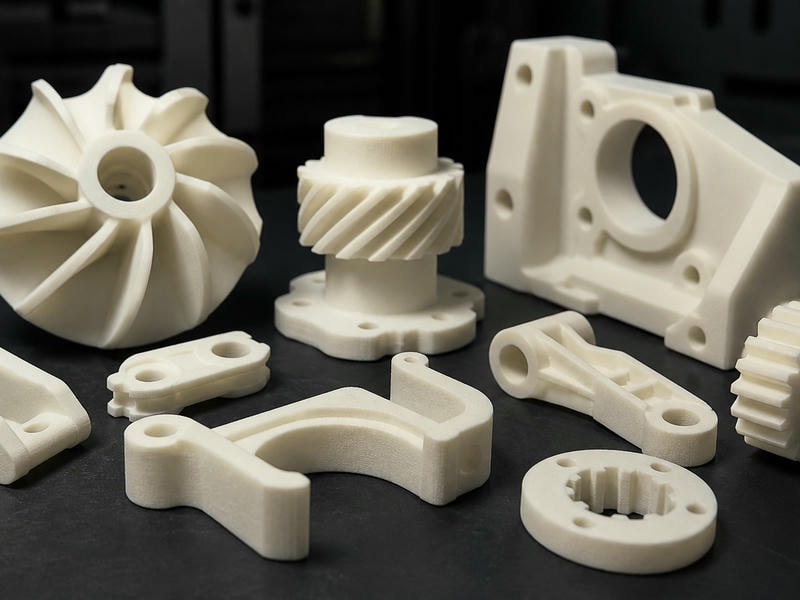
Custom PA (Nylon) 3D Printing Services | Plasticpartsmfg
Get professional PA (Nylon) 3D printing services for functional prototypes and low-volume parts. SLS, MJF, and FDM capabilities for durable engineering components.
View details →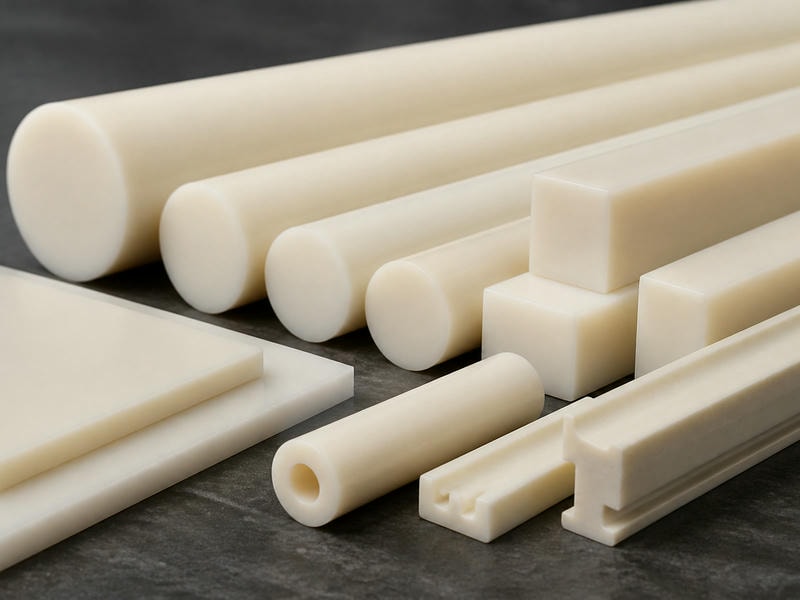
PA Extrusion Molding Services | Custom Nylon Profiles & Tubing | Plasticpartsmfg
Plasticpartsmfg provides custom PA (Nylon) extrusion molding for industrial profiles, tubing, and custom shapes. Precision manufacturing from Shenzhen. Upload your CAD for a quote.
View details →Overcoming Nylon Machining & Molding Challenges
Polyamide polymers are susceptible to hygroscopic expansion, thermal relaxation, and internal stresses caused by high cutting temperatures. Plasticpartsmfg implements structured engineering protocols to protect critical drawing dimensions:
Raw Material Moisture Stabilization
Raw resins and extruded stock are pre-conditioned and dried in dehumidifying ovens prior to milling or injection, mitigating hydrolysis and post-mold shrinkage.
Dedicated Tooling & Heat Dissipation
Polished carbide and PCD cutting tools with high rake angles prevent melting, burr formation, and thread peeling on precision tapped holes.
CMM Dimensional Verification
Parts are stabilized at room temperature before quality checks. Coordinate Measuring Machines (CMM) and optical comparators verify true positions and hole diameters against your 2D print.
Industries Specifying Custom PA Components
Silent gears, timing pulleys, chain guides, and wear pads requiring self-lubrication.
Engine brackets, cable clips, sensor housings, and oil-resistant reservoirs.
Flanged bushings, bearing cages, conveyor links, and insulating spacers.
High-impact power tool enclosures, latching mechanisms, and snap-fit assemblies.
Engineering Tip: For snap-fit assemblies, we recommend unreinforced PA6 or PA12 to maximize elongation at break, whereas glass-filled PA66 is optimized for structural enclosures needing maximum flexural modulus.
Request a Custom PA Quotation
Submit your CAD files, material grades (PA6, PA66, PA12, or reinforced), quantities, and target delivery requirements. Our engineering team in Shenzhen will conduct a DFM review and reply with a complete quotation within 24 hours.