ABS Thermoforming & Vacuum Forming Services
Plasticpartsmfg provides custom ABS thermoforming and vacuum forming services for prototypes, functional engineering parts, low-volume production, and repeat manufacturing. From single validation parts to recurring industrial batches, we deliver complete solutions from DFM and tooling through CNC trimming, finishing, and assembly.
Engineering Capabilities & Specifications
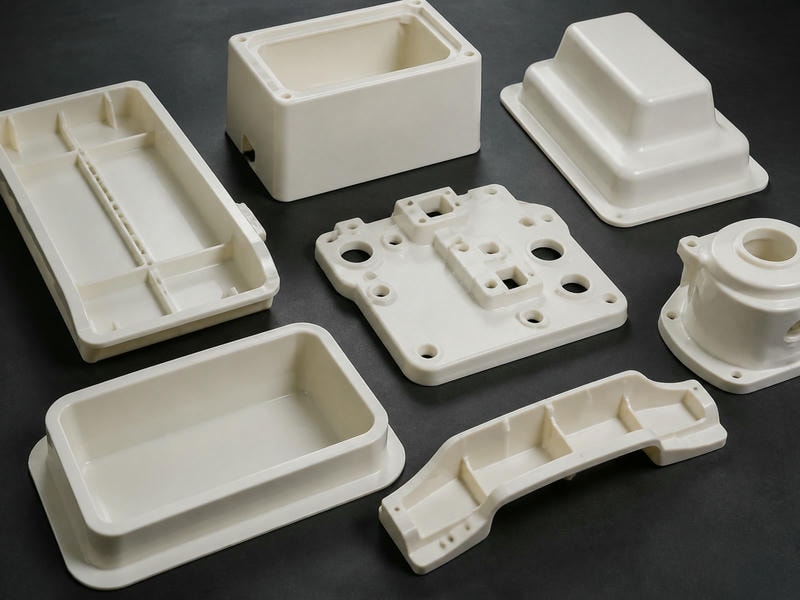
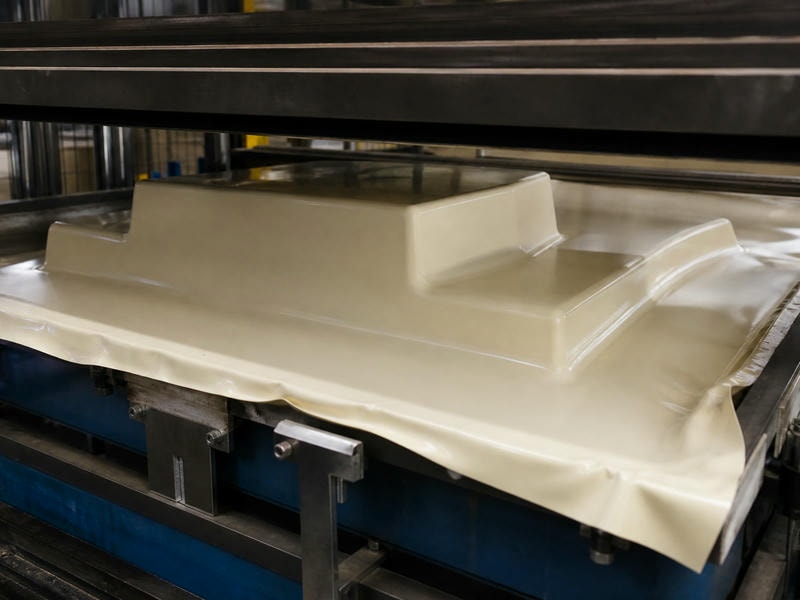
We form heated ABS plastic sheet over high-precision tooling, followed by automated or 5-axis CNC trimming to create lightweight, rigid shells without the heavy capital expense of steel injection tooling.
Forming Methods
Industrial vacuum forming, heavy-gauge sheet thermoforming, and pressure-assisted forming suited for deep draws and crisp contours.
- • Thin to heavy gauge ABS
- • Flame-retardant (UL94-V0) options
Tooling Solutions
CNC-machined aluminum tools for high repeatability, polyurethane/epoxy resin boards for short runs, and additive tooling for pilot validation.
- • Aluminum & composite tooling
- • Dedicated trimming fixtures
Post-Processing & Assembly
5-axis routing, slot cutouts, ultrasonic bonding, threaded insert installation, conductive shielding, surface painting, and screen printing.
- • Tight aperture tolerances
- • Turnkey mechanical integration
| Capability Dimension | Operational Scope & Tolerance Limits |
|---|---|
| Raw Material Formats | Standard ABS, Flame-Retardant ABS, Textured Haircell/Pinseal, Smooth Gloss/Matte, UV-Stabilized |
| Sheet Thickness Range | 1.0 mm to 6.0 mm standard; project-specific assessment available for lighter or heavier profiles |
| Supported File Formats | STEP, STP, IGES, X_T, STL, DXF, DWG, PDF drawings |
| Production Quantities | Prototyping (1-10 pcs), Low-Volume Pilot (20-100 pcs), Recurring Bridge Production (100-1000+ pcs) |
| Dimensional Tolerances | Formed contours: ±0.5 mm to ±1.0 mm depending on draw; CNC trimmed edges and apertures: ±0.2 mm |
Industrial Applications for Formed ABS Components
ABS balances mechanical toughness, surface aesthetics, and cost efficiency. It is the preferred substrate when sheet components require structural stiffness, impact resistance, and a finished aesthetic appearance without costly injection molds.
Equipment Shells & Enclosures
Durable protective guards, diagnostic console bezels, and automation machine housings.
Automotive & Transit Panels
Interior trim, dash surrounds, protective under-dash paneling, and utility vehicle fascias.
Medical & Lab Casings
Ergonomic exterior shells, sanitized instrument covers, and modular display surrounds.
Trays & Handling Fixtures
Heavy-duty transport pallets, specialized electronics carriers, and component organizers.
DFM & Tooling Design Guidelines
Vacuum forming involves heat-induced sheet elongation. Selecting proper geometry safeguards against excessive thinning, unreleased drafts, and localized stress. Click through each guideline to review technical recommendations.
Wall Thickness & Elongation Management
The starting ABS sheet possesses constant gauge, but stretching over tall mold contours causes thinning along vertical walls and deep pocket bottoms. We analyze the draw depth ratio during DFM to specify starting thickness (e.g., 3mm starting gauge yielding ~1.8mm at the deepest draw) to ensure end-use structural integrity.
Process Comparison: Thermoforming vs. Alternatives
Selecting the correct fabrication route balances upfront tooling investment, volume requirements, and dimensional details. We support multiple plastic methods to ensure your components are matched with the most cost-effective process.
| Manufacturing Method | Optimal Volume | Tooling Investment | Lead Time to Parts | Primary Benefit |
|---|---|---|---|---|
| ABS Vacuum / Thermoforming | 10 – 1,000+ units | Low to Moderate ($$) | 1 to 2 Weeks | Large shell parts without high steel tooling investment |
| CNC Machining ABS | 1 – 50 units | None ($) | 3 to 5 Days | Highest positional precision; ideal for thick solid parts |
| Polyurethane Vacuum Casting | 10 – 50 units | Low ($$) | 7 to 10 Days | Complex internal bosses and snap fits on cosmetic prototypes |
| Plastic Injection Molding | 1,000 – 100,000+ | High ($$$$) | 4 to 6 Weeks | Lowest recurring part unit cost at scale with complex molded features |
| Industrial 3D Printing (FDM/SLS) | 1 – 10 units | None ($) | 2 to 4 Days | Rapid verification of complex internals before tooling commitment |
End-to-End Manufacturing Workflow
Our structured project management ensures design feasibility, cost transparency, and continuous dimensional validation from initial CAD analysis to volume dispatch.
DFM & Tool Engineering
CAD evaluation for draw ratios, draft clearances, tool shrink allowances, and trim perimeter paths.
Tooling Fabrication
High-speed CNC milling of aluminum or composite molds alongside custom trimming routing nests.
Trial Forming & Trimming
Sample forming, automated 5-axis CNC trimming of features, and dimensional sign-off against drawings.
Secondary Ops & Batch Run
Serial thermoforming, post-finishing (bonding, painting, screen print), packaging, and door-to-door freight.
Request a Quotation for ABS Thermoforming
Send your drawings and specifications for a practical manufacturing evaluation and pricing breakdown. Our engineers will verify sheet draw feasibility, suggest the optimal tooling strategy, and quote competitive production lead times.
Information Checklist for Fast RFQ
- • 3D CAD & 2D Drawings: STEP, STP, or IGES with critical tolerances noted.
- • ABS Sheet Specification: Target thickness (1.0–6.0mm), grade (FR/standard), color, and surface texture.
- • Quantities: Target prototype count and anticipated pilot batch volume.
- • Secondary Demands: Threaded inserts, assembly requirements, painting, or silk-screening.
Direct Inquiries:
Facility: