Low-Volume Rotational Molding Services
Plasticpartsmfg delivers professional rotational molding solutions in Shenzhen, China, built specifically for prototype-to-production runs and bridge manufacturing. Transition large-scale, complex hollow components from CAD to functional reality without the capital burden of heavy injection tooling.
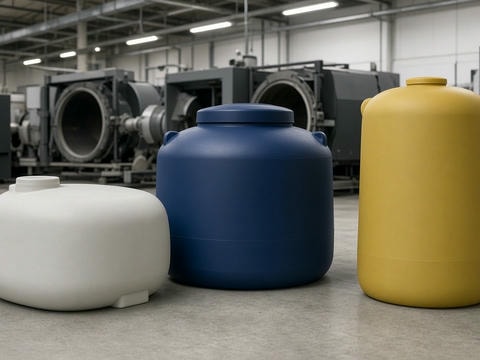
Why Rotational Molding for Low-Volume Production?
Rotational molding uses bi-axial low-speed rotation in a heated oven to coat mold walls evenly. This produces hollow parts free from the internal stresses inherent to high-pressure injection molding.
Cost-Effective Tooling
Fabricated sheet metal or cast aluminum tooling is dramatically less expensive than high-pressure steel molds, preserving capital on low-volume and bridge runs.
Uniform Wall Thickness
Centrifugal-free distribution ensures consistent wall thickness across complex geometry, reinforcing corners and structural radii naturally.
Stress-Free Parts
Because polymers fuse under gravity and ambient pressure rather than high velocity, parts exhibit superior impact resistance and resistance to environmental stress cracking.
Broad Design Freedom
Seamlessly produce complex hollow profiles, dual-walled enclosures, and multi-undercut designs that are impossible or cost-prohibitive via traditional machining or blow molding.
Technical Capabilities & Specifications
From quick-turn tooling modifications to final assembly, our rotomolding shop operates with strict adherence to engineering tolerance targets and batch-to-batch consistency.
| Capability | Specification |
|---|---|
| Process | Bi-Axial Rotational Molding (Rotomolding) |
| Supported Resins | LLDPE, HDPE, XLPE (Cross-linked), PP |
| Batch Quantities | Prototype, Pilot Batches, Low-Volume Production |
| Wall Thickness | Typically 2mm – 10mm (geometry dependent) |
| Dimensional Tolerance | ±1% to ±3% of nominal dimension |
| Surface Finishes | Matte, Mold-Tech Textures, Custom Tool Finishes |
| Secondary Operations | CNC Trimming, Routing, Spin-Weld & Threaded Inserts, Assembly |
Resin & Polymer Selection
Selection of rotomolding powder grades is tailored to operational temperatures, chemical exposure, and mechanical load profiles.
LLDPE (Linear Low-Density Polyethylene)
The primary workhorse for hollow parts. Combines high tensile elongation, broad impact resistance across ambient temperatures, and predictable shrinkage behavior.
HDPE (High-Density Polyethylene)
Enhanced stiffness and hardness suitable for structural containers, aggressive chemical sumps, and rigid industrial tanks requiring high flexural modulus.
XLPE (Cross-Linked Polyethylene)
Formulated for severe applications requiring exceptional environmental stress crack resistance (ESCR), extreme cold-weather impact resilience, and high chemical compatibility.
Custom Additives & Compounding
UV stabilization (UV8/UV20), FDA food-contact compliance, custom pigment masterbatching, anti-static compounds, and UL94 flame-retardant packages.
Target Applications & Secondary Operations
Rotational molding shines across large-envelope parts requiring structural endurance without secondary joints or adhesive seams.
Containers & Fluid Tanks
Integrated diesel, DEF, and potable water reservoirs. Seamless construction guarantees 100% leak-proof performance under cyclical hydrostatic loads.
Housings & Machinery Enclosures
Protective enclosures for commercial sweepers, diagnostic equipment, agricultural machinery, and outdoor electrical infrastructure requiring high impact tolerance.
Specialized Material Handling Bins
Double-walled insulated totes, reusable bulk transit bins, and ruggedized instrument shipping cases engineered for repeated forklift and pallet handling.
Large HVAC & Fluid Ducting
Complex curved routing channels, air intake transitions, and under-hood ducts that eliminate assembly hardware and pressure drops.
Recreational & Heavy Duty Structures
Playground components, marine buoys, floats, and durable barrier structures built to withstand continuous UV exposure and harsh weather.
Turnkey Secondary Operations
In-house precision CNC trimming, mold-in brass inserts, spin-welded threaded fittings, custom drilling, gasket installation, and hardware assembly.
Quality Control & Inspection System
Our production methodology couples real-time process monitoring with disciplined quality assurance to ensure reliable fit and mechanical performance.
Dimensional Verification
Critical mounting interfaces, hole patterns, and exterior footprints are validated directly against your 3D CAD models using calibrated gauging and coordinate check points.
Wall Thickness Gauging
Ultrasonic thickness testing is performed systematically on corners, deep draws, and structural ribs to guarantee adherence to minimal wall requirements.
Material Traceability
Full lot traceability with resin certificates of analysis (CoA), verifying raw virgin pellet compliance, melt flow index (MFI), and additive dispersion.
Aesthetic & Seal Integrity
Inspection of parting line flushness, visual surface uniformity, bubble entrapment audits, and pressure testing for all closed liquid vessel applications.
How to Get Started
Send your design files to our Shenzhen engineering team for DFM feedback, tooling timeline estimations, and low-volume production quotations.
Recommended Submission Details:
- 1. 3D CAD Files: STEP, IGS, or native SolidWorks models for mold analysis.
- 2. Material & Color: Desired resin (e.g., LLDPE, HDPE), UV ratings, and color code/RAL.
- 3. Projected Volume: Prototype batch size and anticipated annual quantities.
- 4. Secondary Scope: Threaded insert locations, post-mold machining, or hardware fitments.